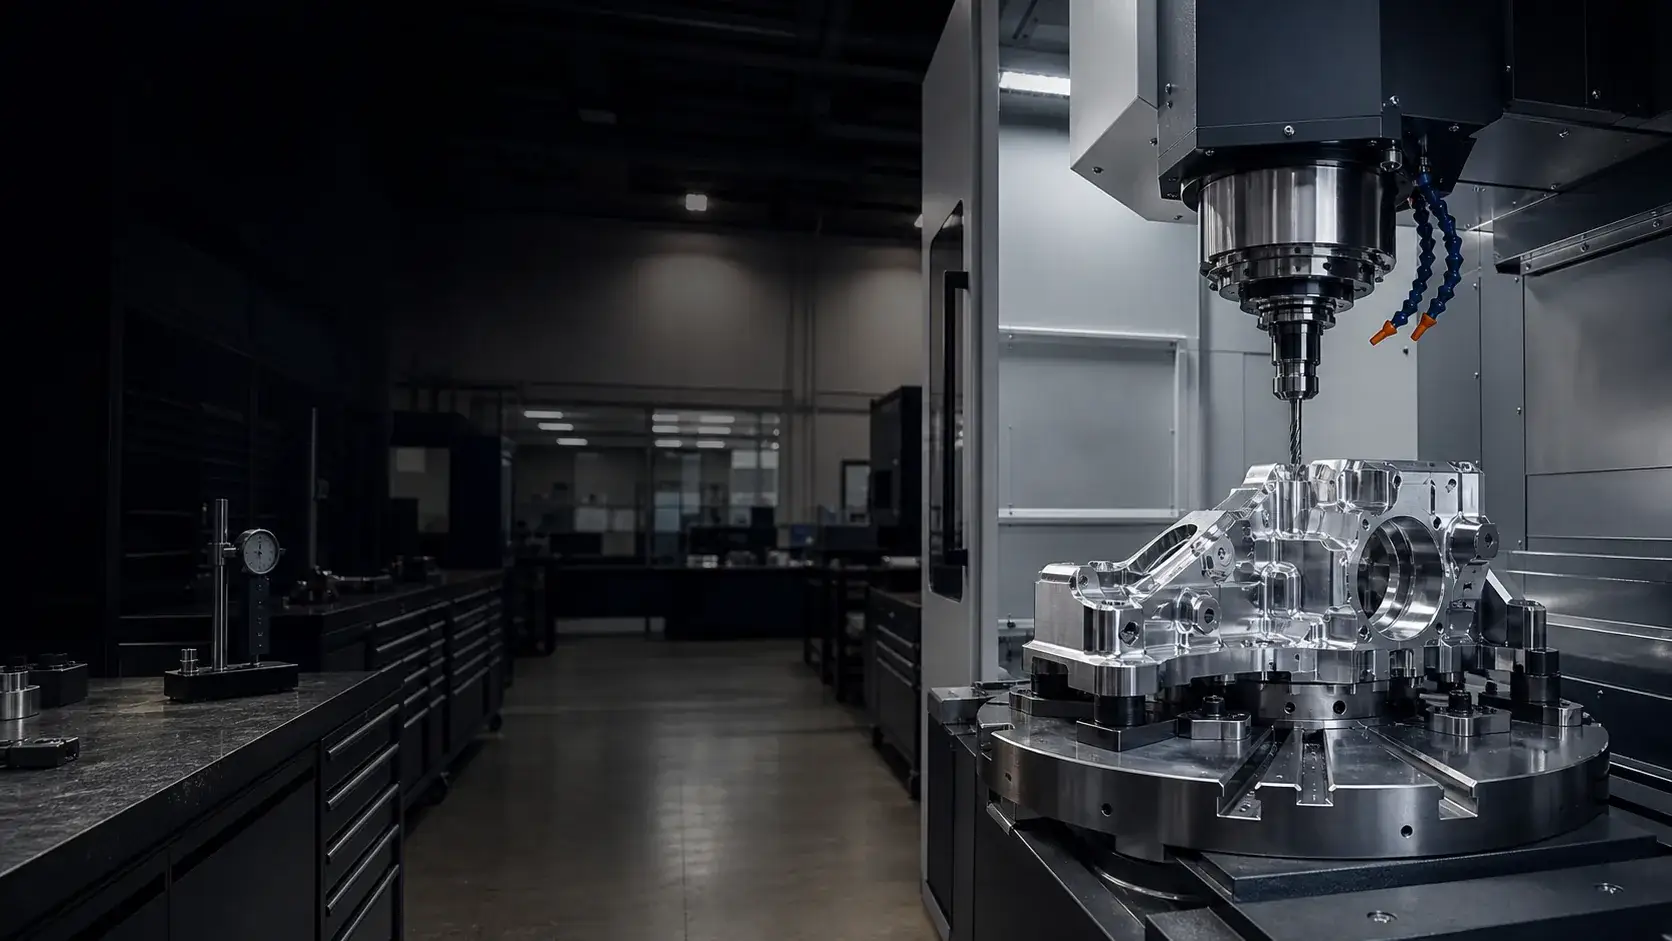
Setups, tooling, and in-process checks are defined before production so results are repeatable, not lucky.
Quality assurance
Quality Assurance for Precision Aluminum CNC Machining
This is a working reference for how we control quality — from DFM review and material traceability through calibrated inspection and documented results. It is built on evidence you can verify, not claims.
We inspect 6061, 7075, 2024, 5052, and MIC-6 aluminum parts against your drawings with FAI, CMM, and dimensional reporting, and reply to your RFQ within one business day.
- ISO 9001:2015 certified
- First Article Inspection available
- Material certificates available
- Engineering review within one business day
- Prototype to production
Quality philosophy
Quality is planned in, not inspected on
Good measurements start with good decisions. Our approach is built on five things we control on every aluminum job.
We review critical dimensions, datums, and inspection needs during DFM — catching risk before chips are cut.
Critical features are gauged part to part, so the last piece in a batch measures like the first article.
Alloy and temper are traced back to certified stock, with mill certificates available when the order requires them.
If a drawing, process, or measurement needs review, we escalate quickly rather than ship a question mark.
Inspection equipment
Calibrated measurement, from CMM to gauge blocks
Inspection is only as good as the tools behind it. These are the instruments an aluminum part passes through before it ships — photographed on our own floor in inside the factory.
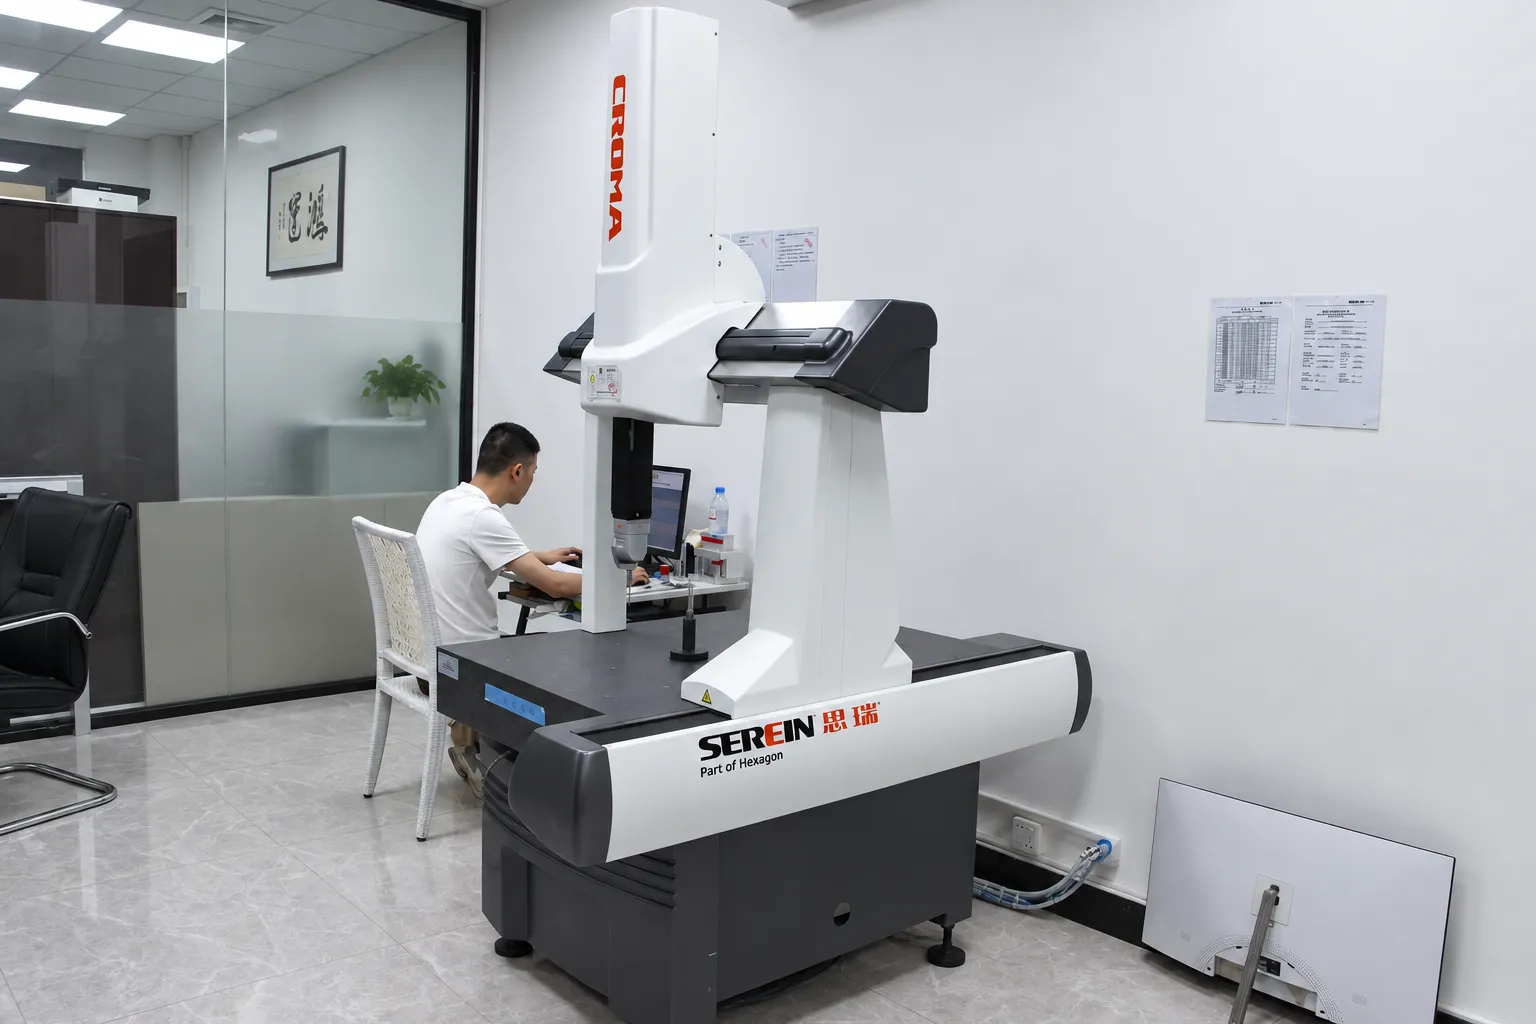
Coordinate Measuring Machine (CMM)
InspectsTrue position, profile, flatness, and complex dimensions beyond hand tools.
Typical useHole patterns, bores, contoured parts, and full FAI dimensional layouts.
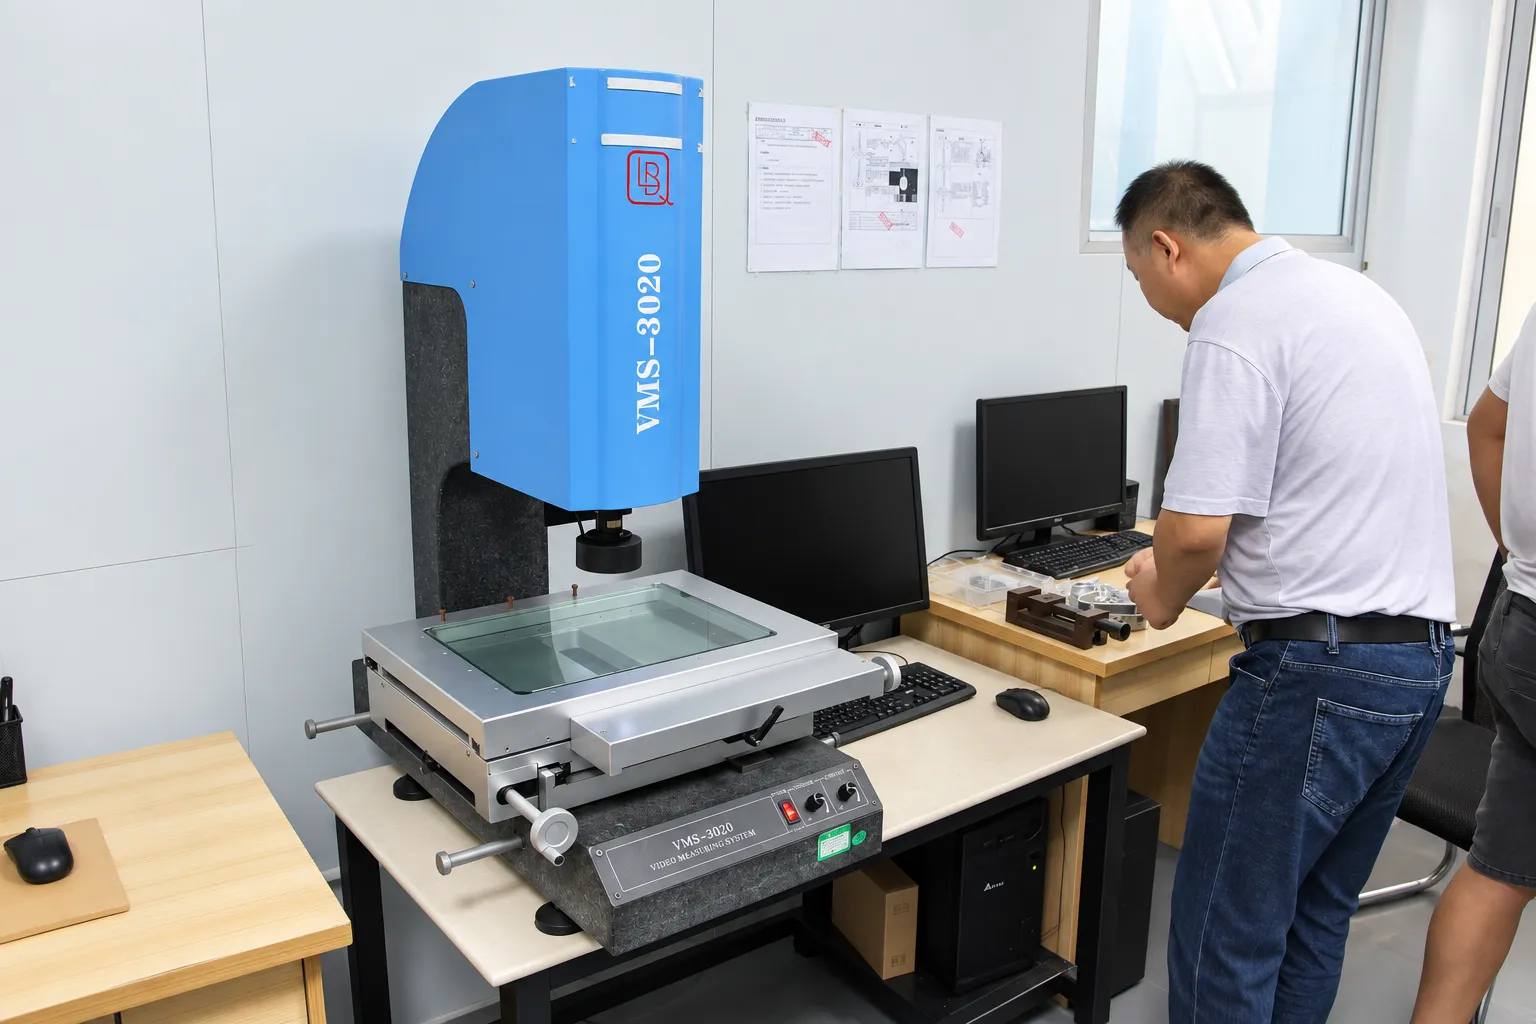
Optical measuring system
InspectsNon-contact measurement of small, delicate, or 2D-profile features.
Typical useThin parts, small hole diameters, edges, and features that contact probes would distort.
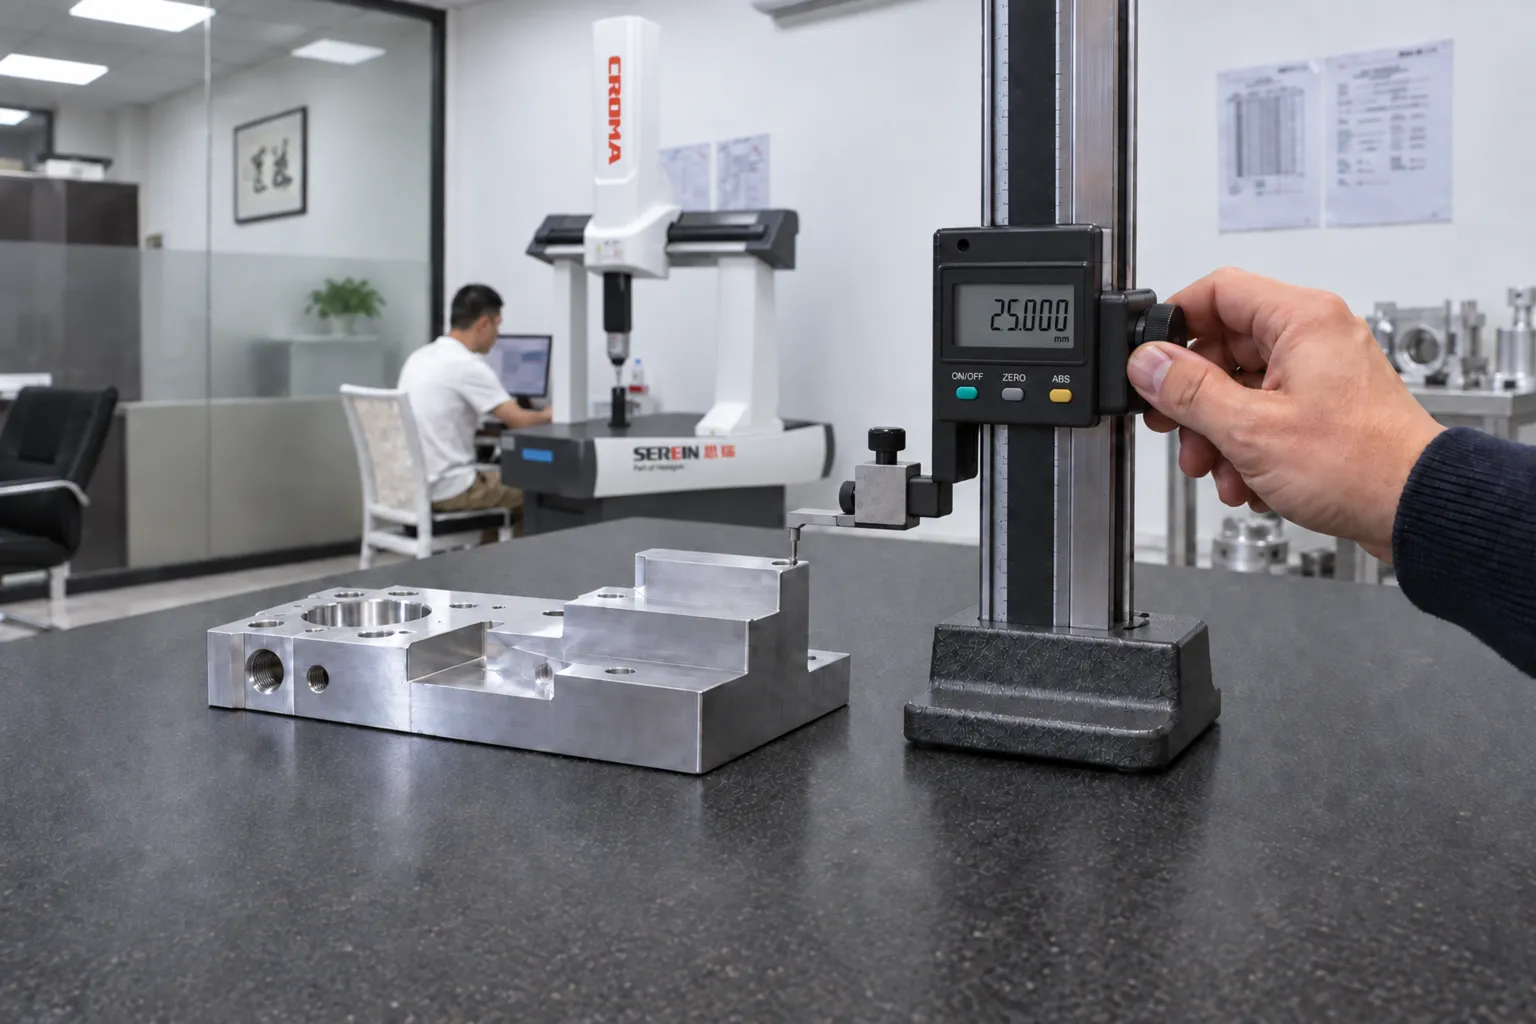
Height gauge
InspectsHeights, steps, and datum-referenced dimensions on a surface plate.
Typical usePrismatic aluminum parts, plates, and layout of machined faces.
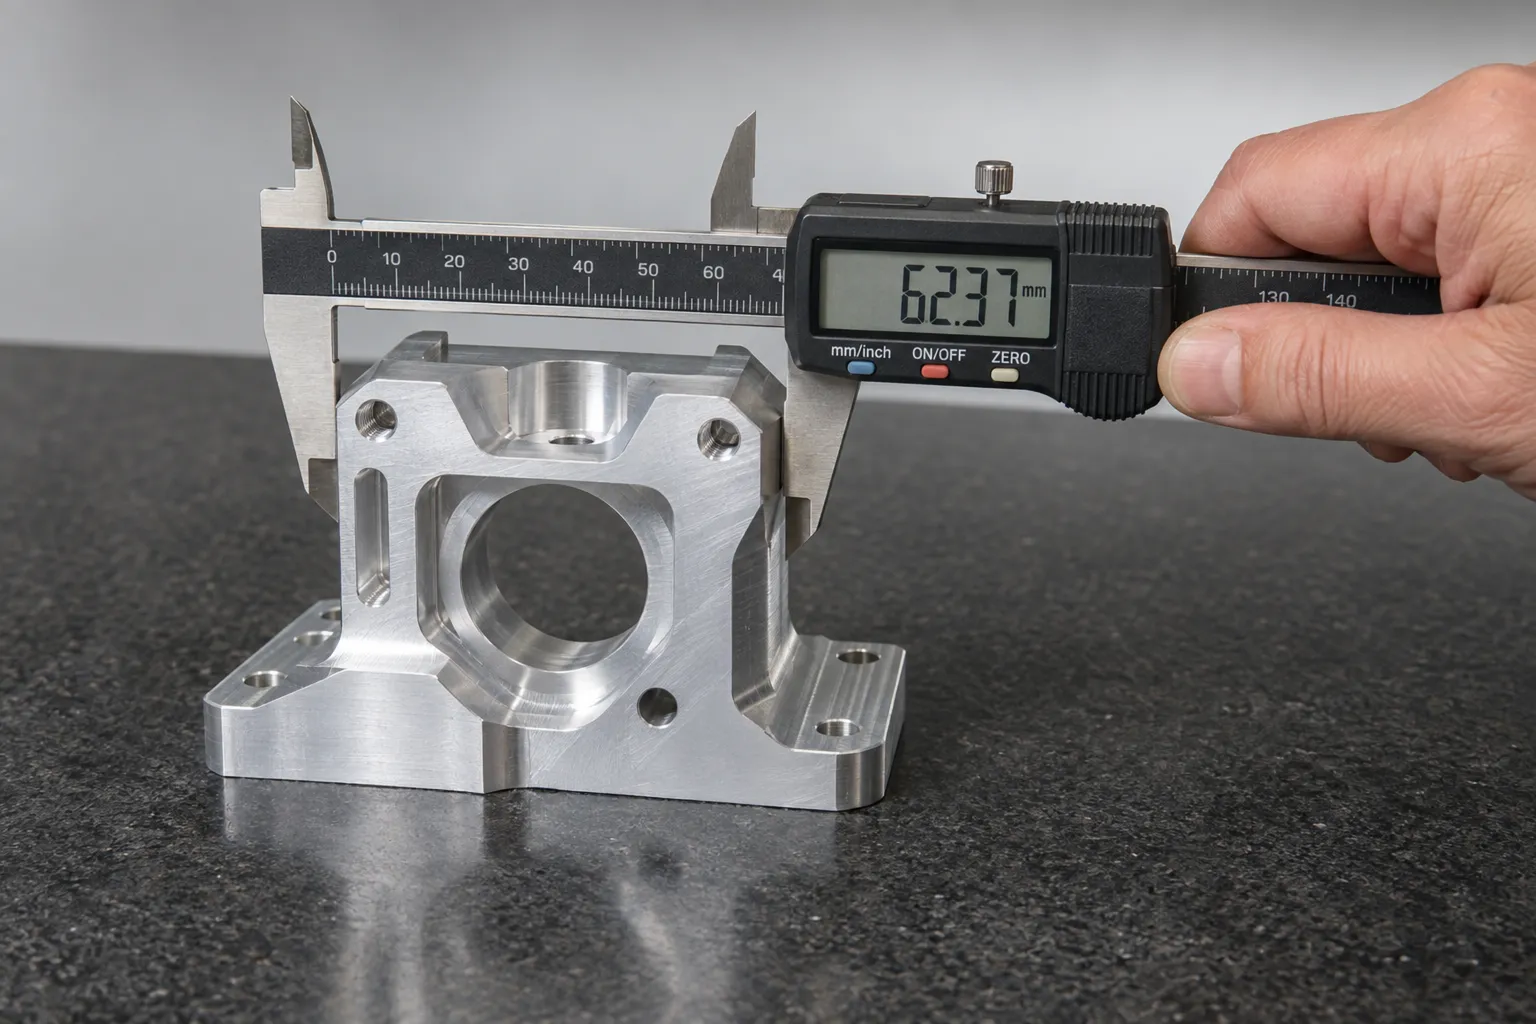
Digital calipers
InspectsGeneral outside, inside, length, and depth measurement.
Typical useFirst-off checks and quick in-process verification across most features.
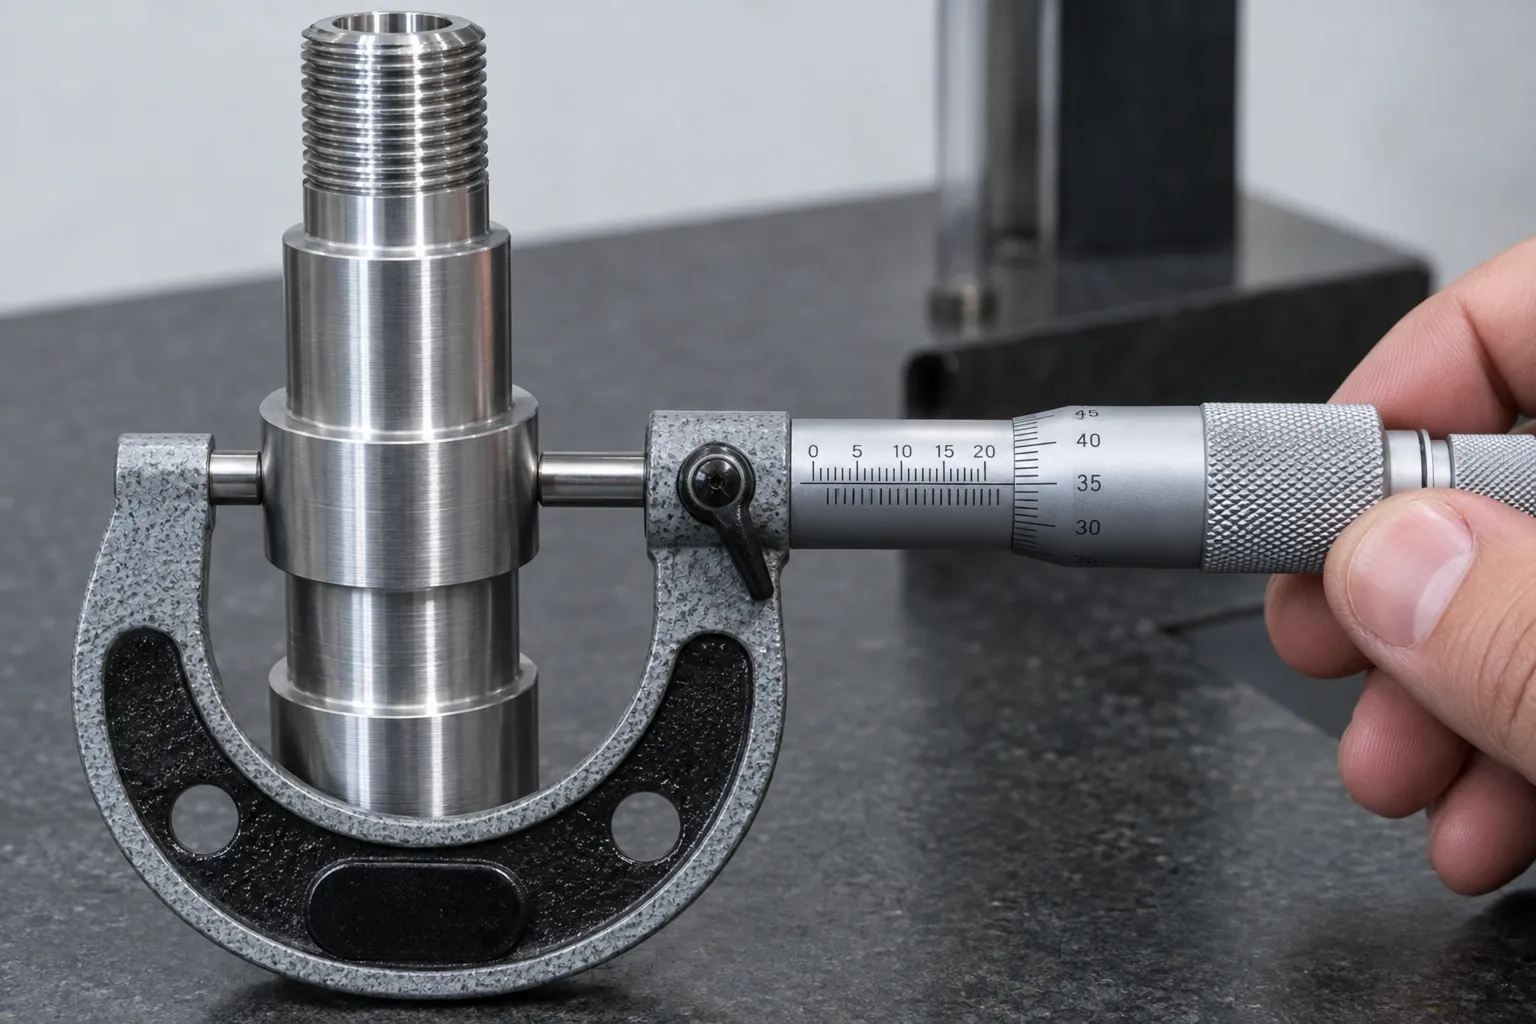
Micrometers
InspectsPrecise outside diameters and thicknesses to close tolerance.
Typical useTurned diameters, wall thickness, and tight dimensional features.
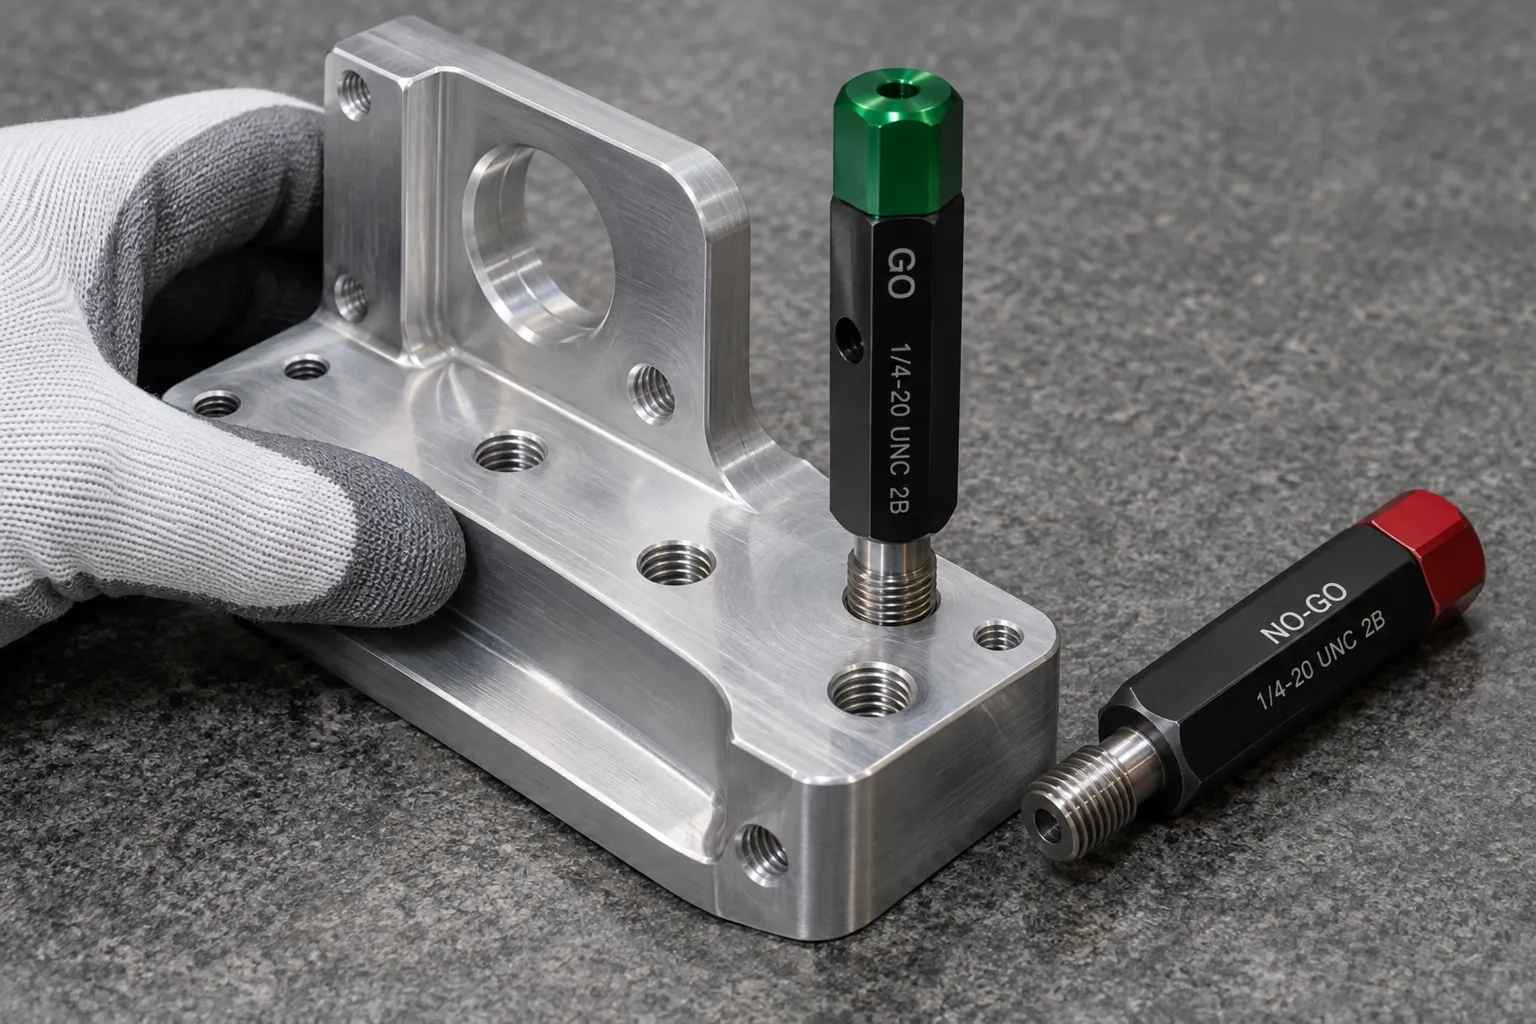
Thread gauges
InspectsGo / no-go verification of thread fit and class.
Typical useTapped holes and turned threads — metric, UNC, and UNF.
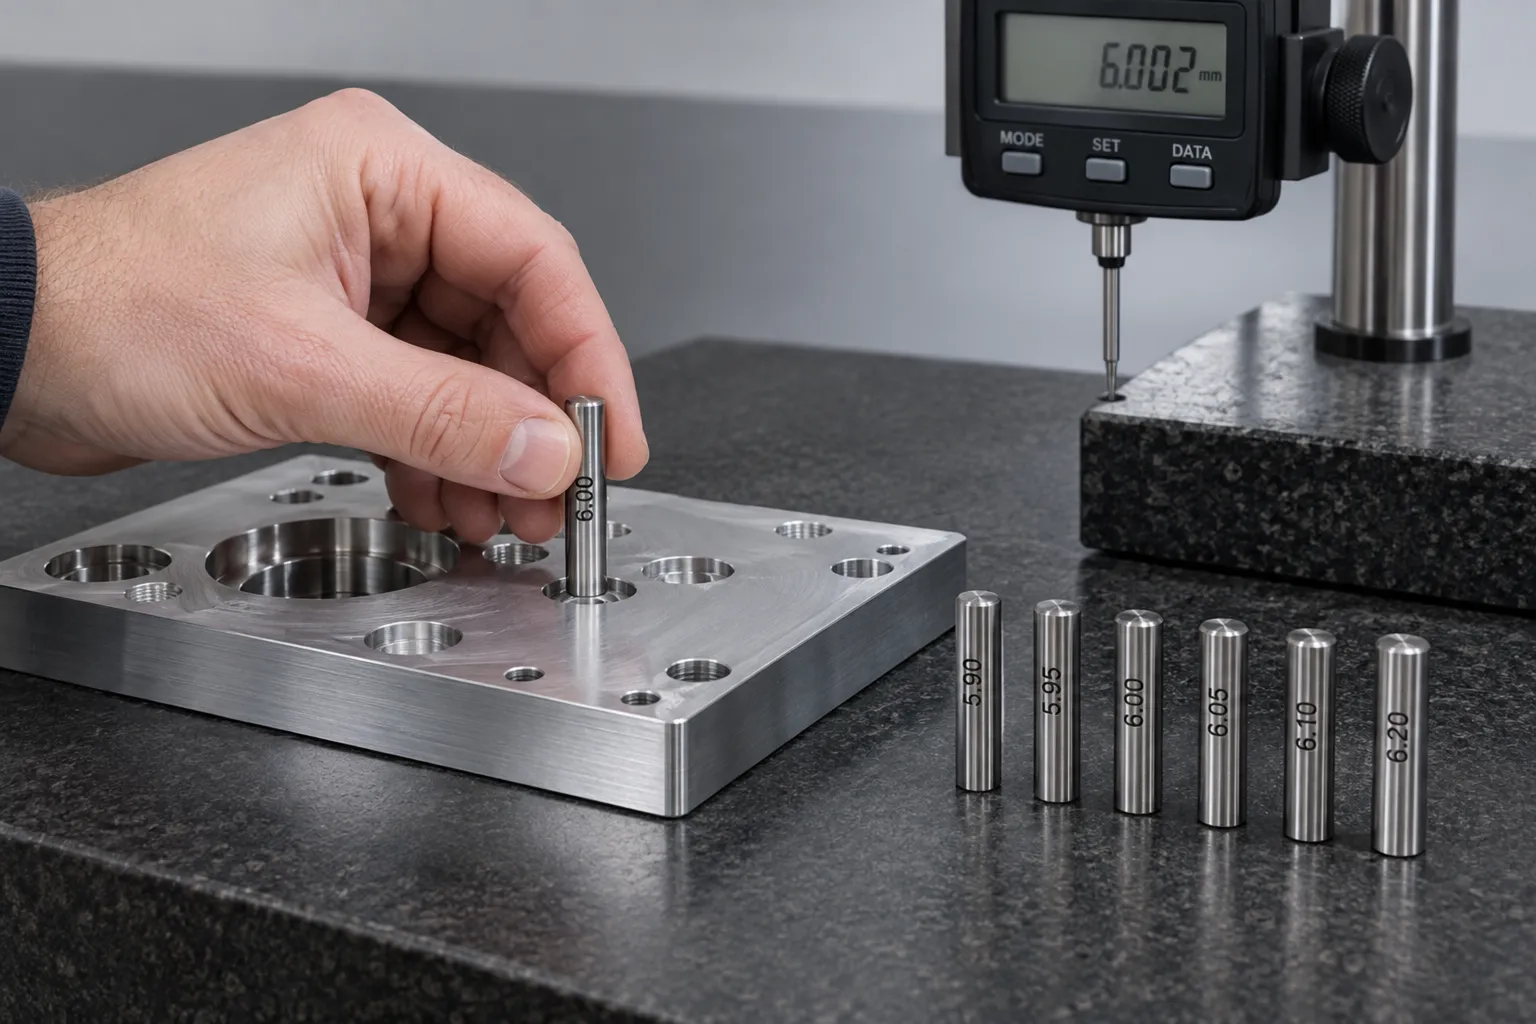
Pin gauges
InspectsHole diameter and go / no-go bore verification.
Typical useReamed holes, dowel bores, and precision hole diameters.
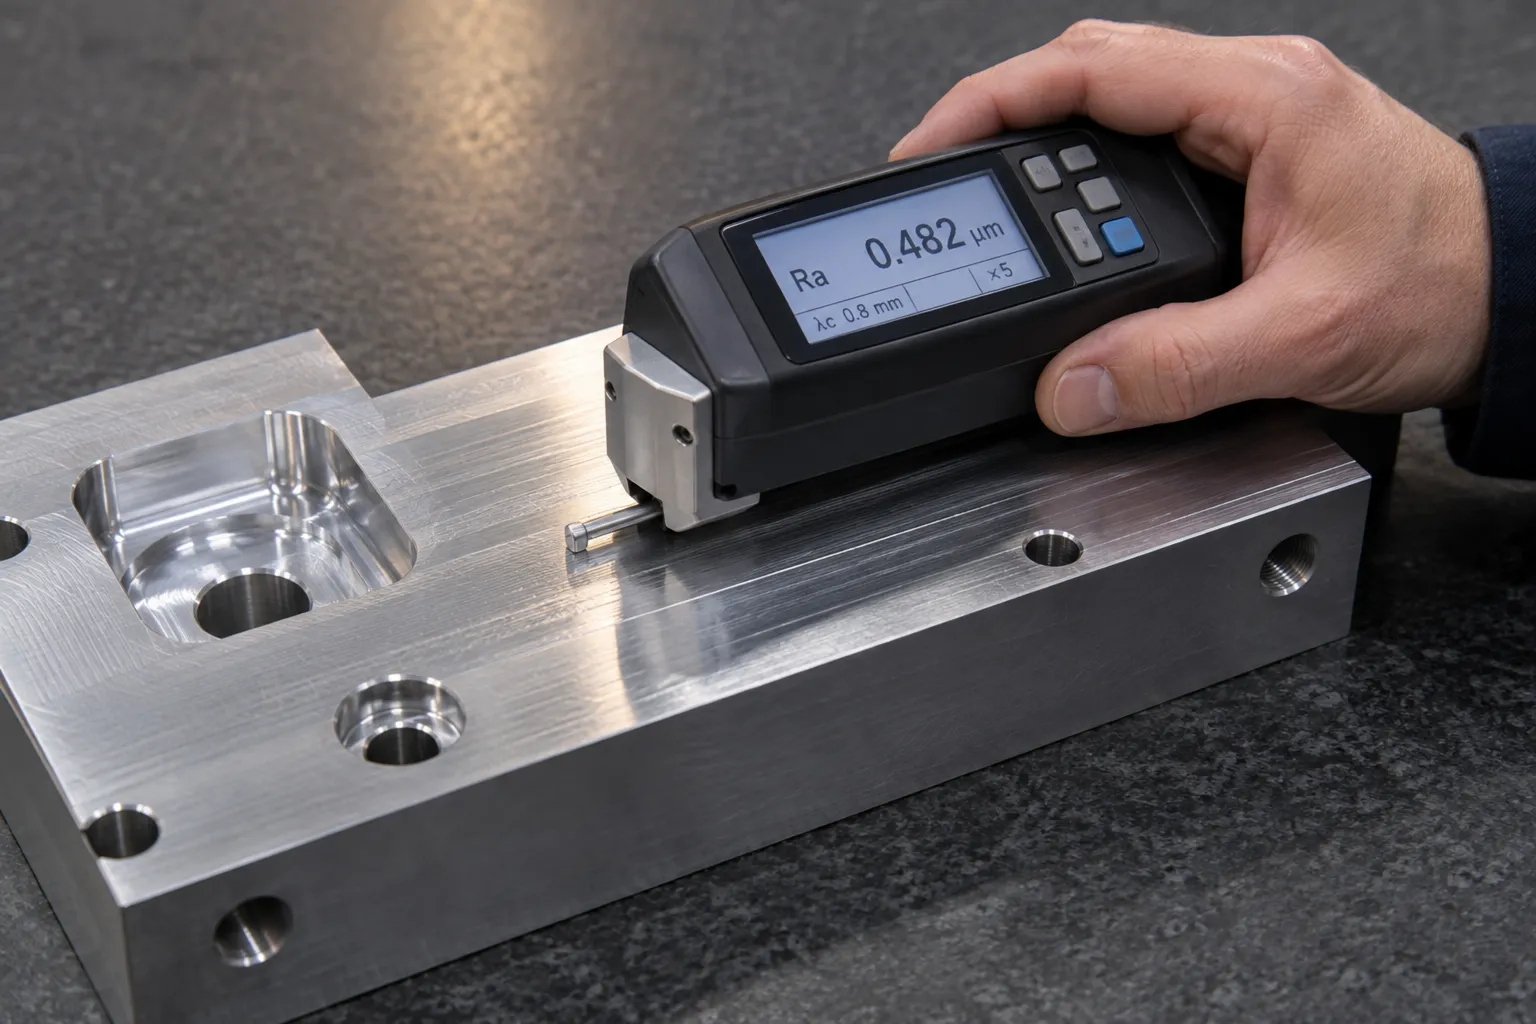
Surface roughness tester
InspectsRa verification against the specified surface finish.
Typical useSealing faces, bearing surfaces, and cosmetic finish acceptance.
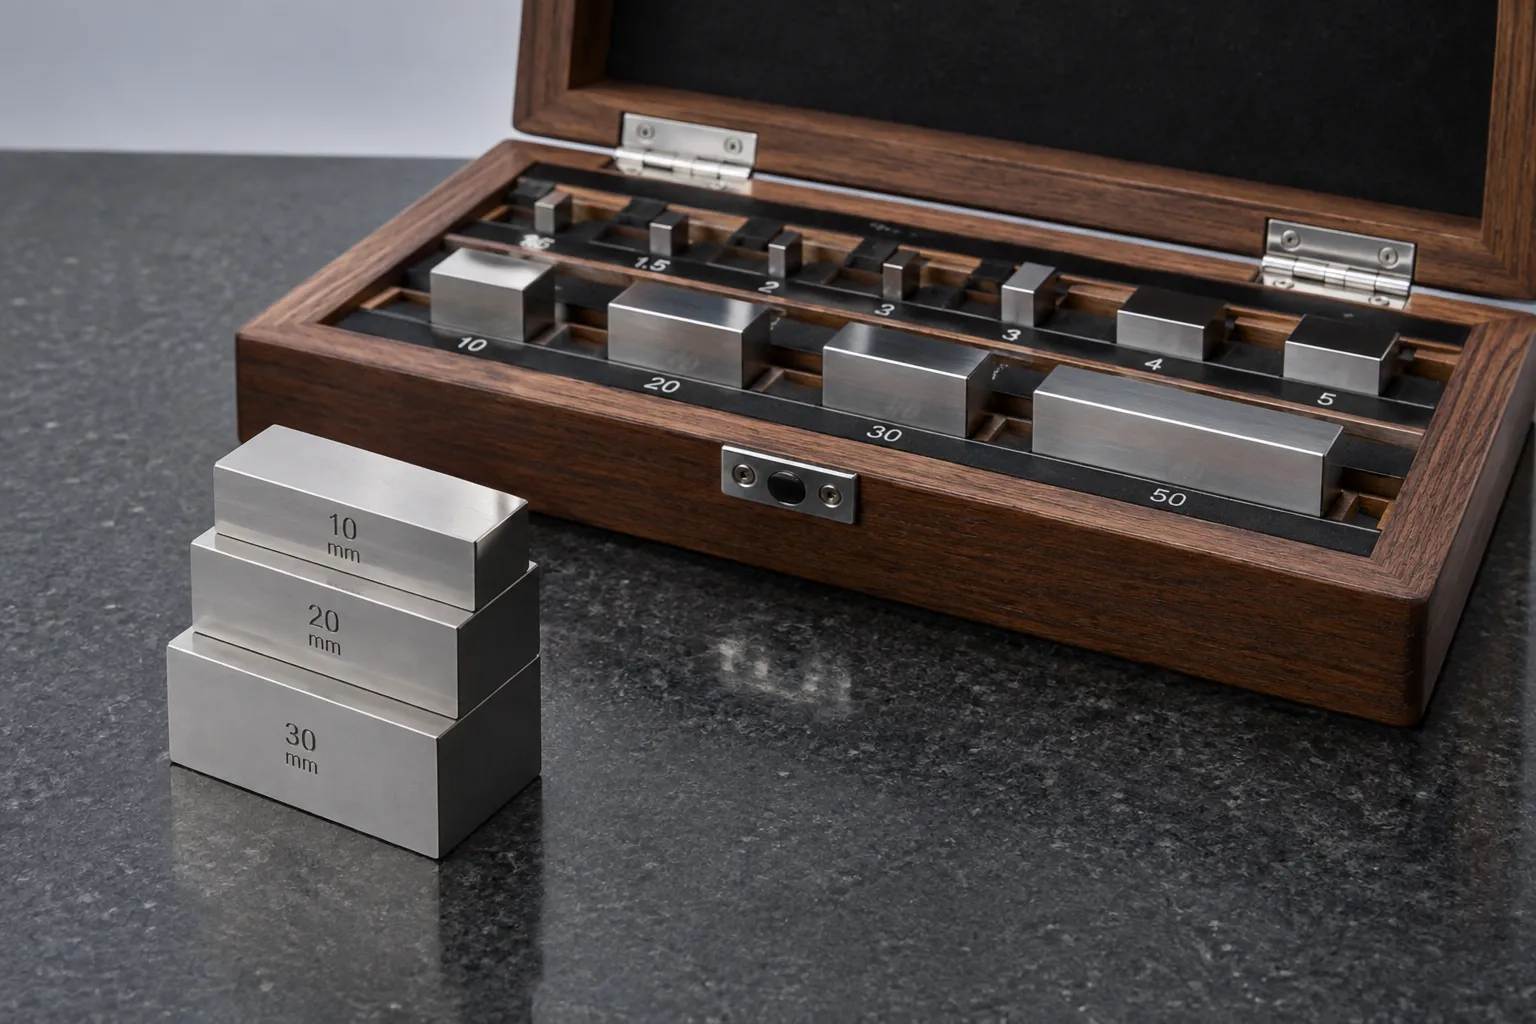
Gauge blocks
InspectsCalibrated reference standards for setting and checking other instruments.
Typical useInstrument calibration and comparative dimensional checks.
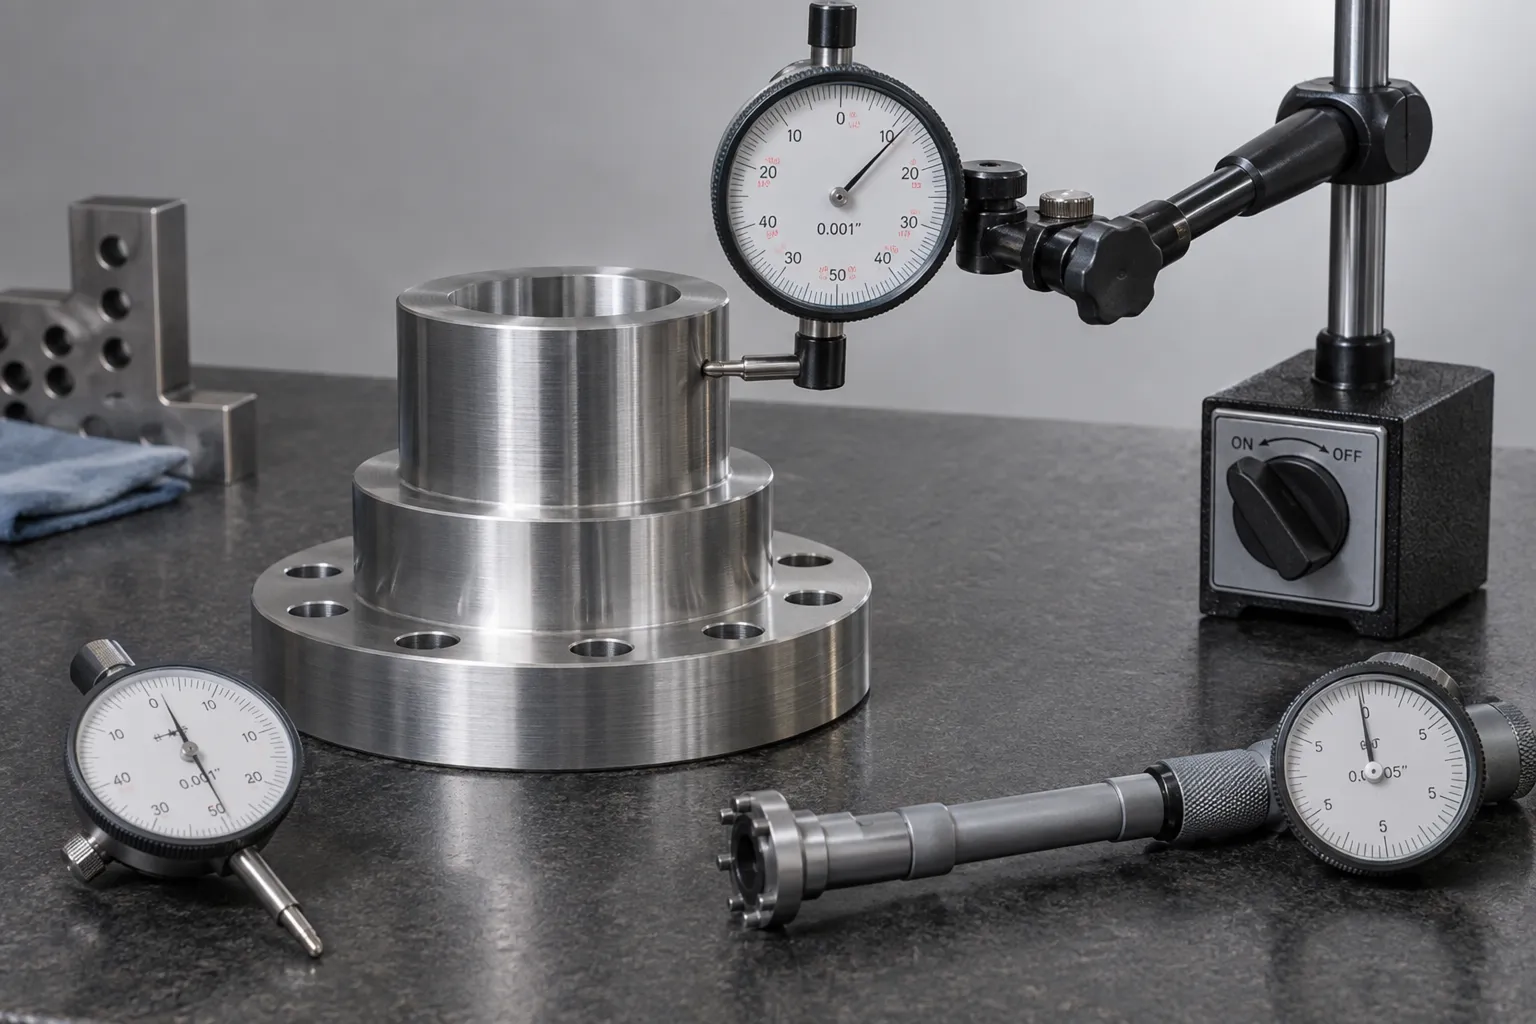
Calibrated hand tools & indicators
InspectsBore gauges, dial indicators, radius and thread-pitch gauges.
Typical useSpecialized feature checks, runout, and comparative measurement.
Sample quality documents
The documentation you receive
These are the records we issue with aluminum parts. Ask for any of them and we will send a redacted example from a past job for your supplier review.
First Article Inspection (FAI) Report
Request a sample
A ballooned drawing with every dimension measured and recorded for sign-off of a new part or revision.
Dimensional Inspection Report
Request a sample
Recorded measurements for critical features and customer-defined checkpoints across a production batch.
Material Certificate
Request a sample
Mill certification tracing the aluminum alloy and temper back to the supplied stock.
Inspection Checklist
Request a sample
The per-part checklist covering dimensions, threads, finish, cosmetics, and packaging before release.
Aluminum-specific quality control
How aluminum parts are actually inspected
Aluminum has its own failure modes — burrs, warping, cosmetic damage, and anodizing variation. This is what we check, how we check it, and what it takes to control.
| Inspection focus | Why it matters | Inspection method | Manufacturing consideration |
|---|---|---|---|
| Burr control | Soft aluminum raises burrs that affect fit, sealing, safety, and downstream assembly. | Visual and tactile edge inspection; magnification on fine features. | Entry chamfers, thread-milling, and controlled deburr or tumbling designed in up front. |
| Thread inspection | Wrong class or damaged threads cause assembly failures and rework. | Go / no-go plug and ring gauges to the specified class of fit. | Tap vs. thread-mill choice and clean chip evacuation in ductile aluminum. |
| Flatness verification | Flatness drives sealing, mating, and datum integrity on plates and bases. | Surface plate with height gauge or indicator; CMM for tight callouts. | Stress-relieved stock, balanced material removal, and low-stress fixturing. |
| Hole position accuracy | True-position error stacks up and misaligns bolt patterns and dowels. | CMM true-position measurement referenced to part datums. | Single-setup drilling, spot-drilling, and a clear datum scheme. |
| Cosmetic surface inspection | Visible faces show handling and tool marks, especially before anodizing. | Controlled-light visual inspection against defined A-surfaces. | Fixturing off non-cosmetic faces and protected handling between operations. |
| Surface roughness verification | Ra affects sealing, wear, adhesion, and cosmetic acceptance. | Calibrated surface roughness tester against the drawing Ra. | Tool path, feed, and finishing passes tuned to the target Ra. |
| Anodizing color consistency | Shade drift between parts or batches is rejected on cosmetic assemblies. | Visual comparison to an approved reference sample under set lighting. | Batching parts together, alloy selection, and consistent surface prep. |
| Film thickness (anodize) | Coating grows dimensions and can bind tight fits and threads. | Coating thickness verification on witness or sampled areas. | Masking threads and tight bores; allowing for build on critical features. |
| Edge quality | Sharp or ragged edges are a safety and fit issue and a cosmetic defect. | Visual and tactile inspection of chamfers, radii, and break edges. | Specified edge breaks and consistent deburring routed away from A-surfaces. |
| Scratch prevention | Aluminum marks easily; scratches ruin cosmetic and anodized parts. | Final visual inspection under controlled light before packing. | Protective film, soft handling, and clean fixtures throughout the flow. |
| Dent prevention | Dings from handling or contact are non-recoverable on finished parts. | Visual and dimensional check of critical and cosmetic faces. | Foam nesting, partitions, and careful inter-operation handling. |
| Surface cleanliness | Coolant, chips, and residue cause corrosion spots and finish defects. | Cleanliness inspection after cleaning and before packaging. | Proper cleaning, drying, and handling before finish and dispatch. |
| Packaging inspection | Damage in transit undoes good machining and inspection. | Check of wrap, foam, partitions, and carton before sealing. | Packaging matched to part fragility, finish, and export conditions. |
Packaging & shipping protection
Finished parts arrive the way they left
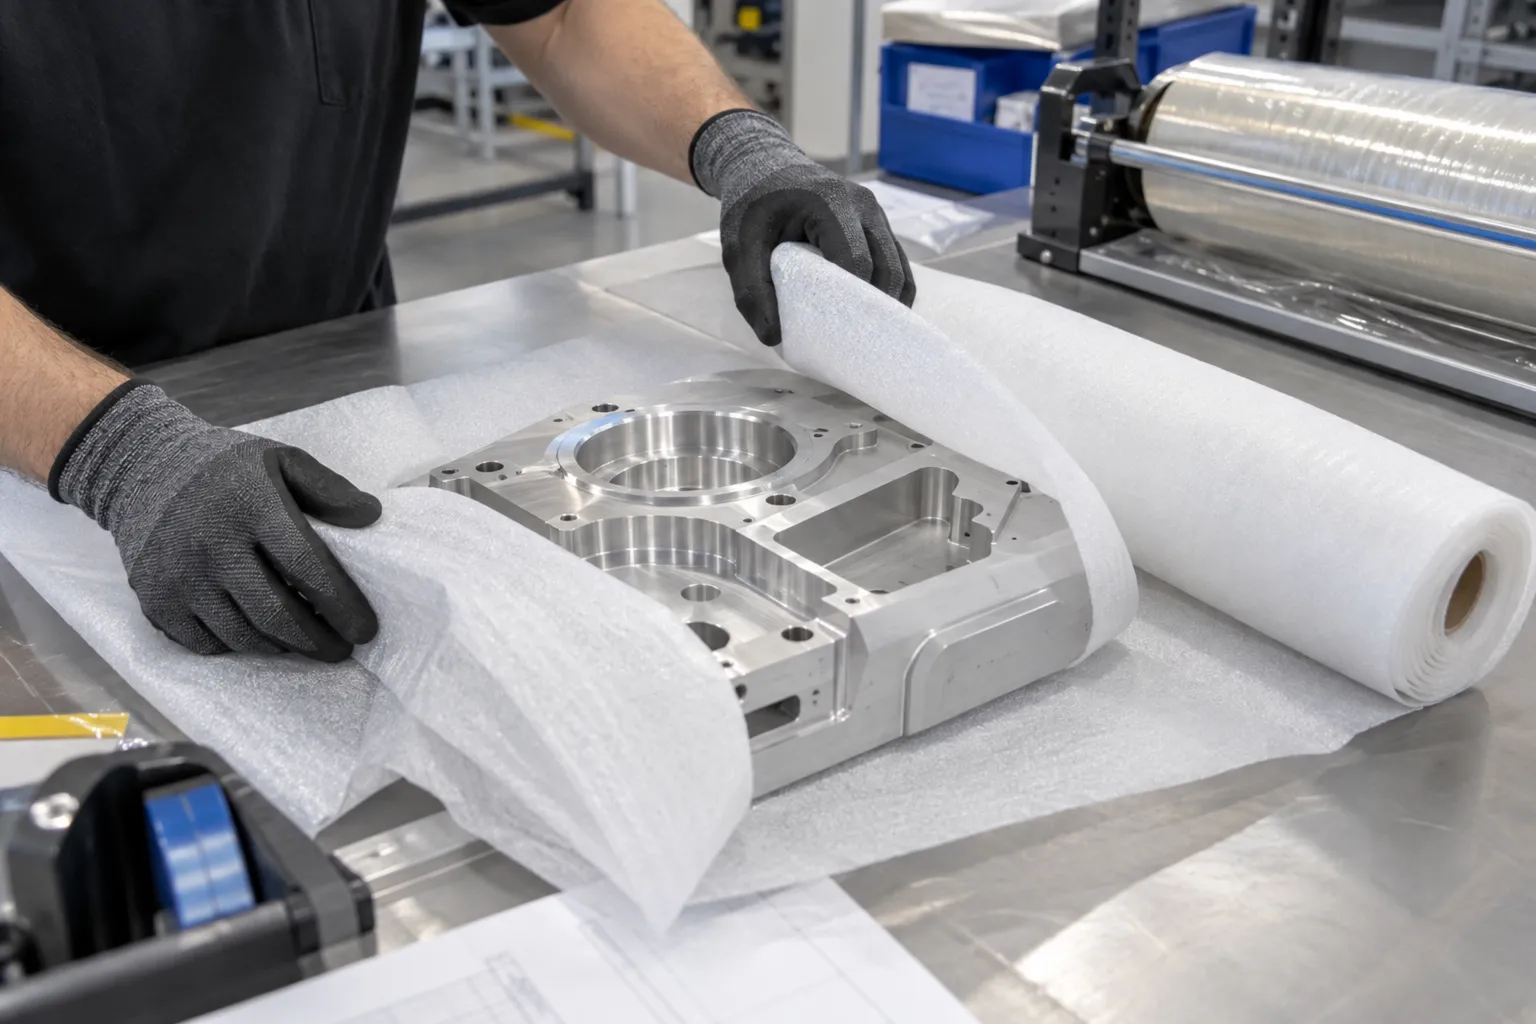
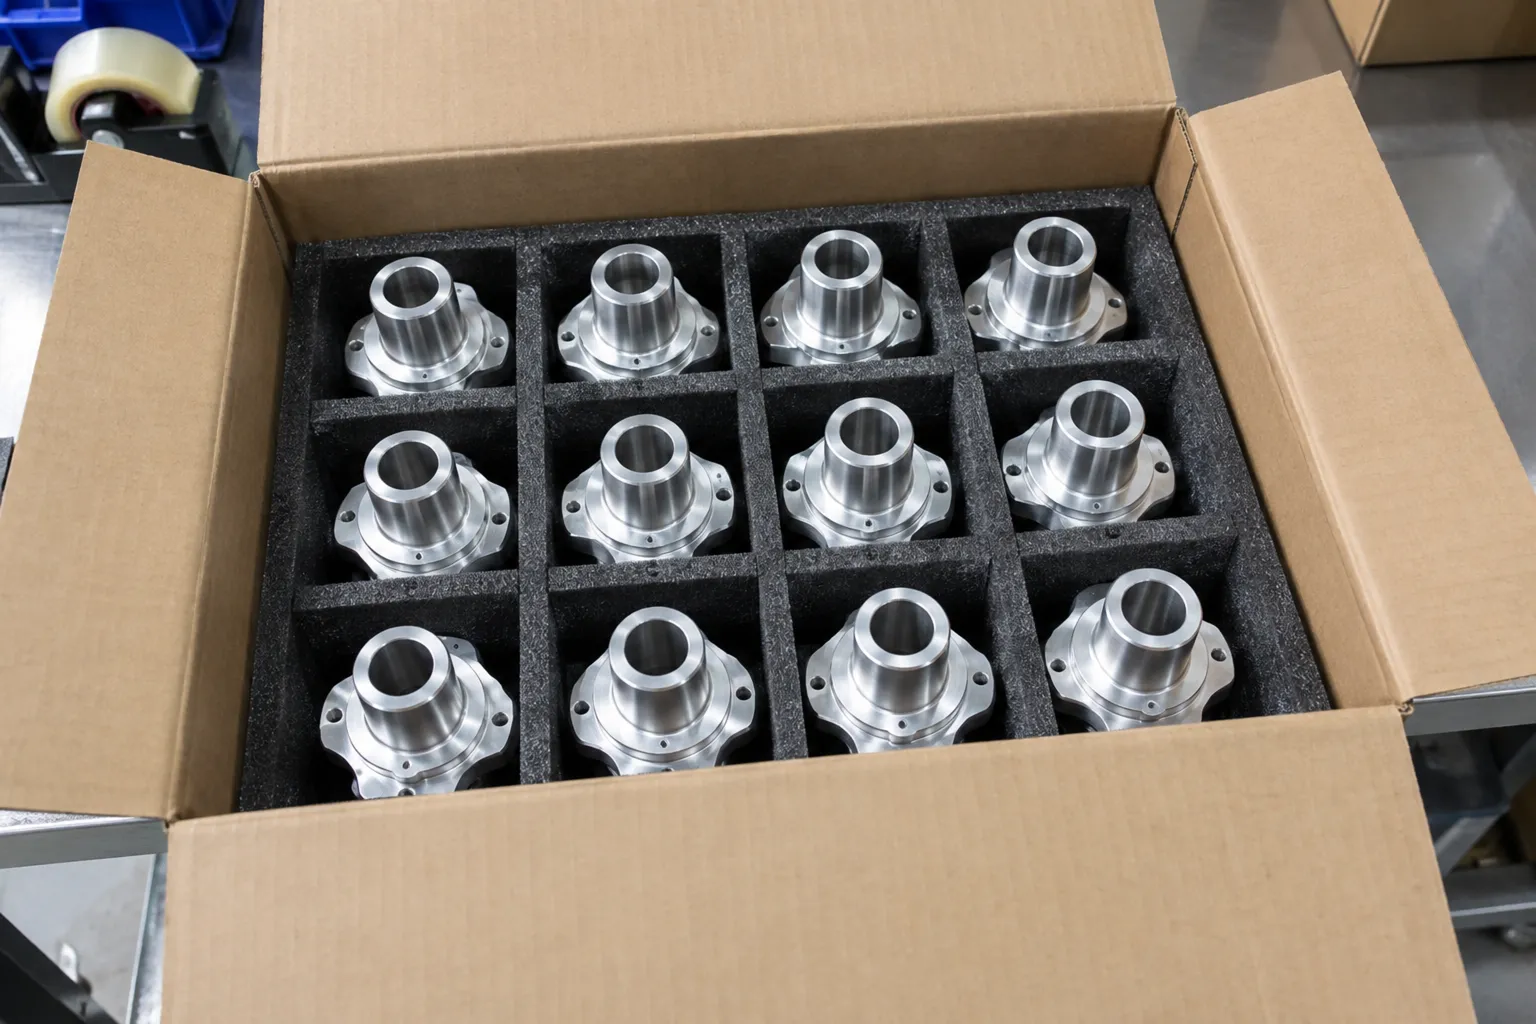
Aluminum marks and dents easily, so packaging is part of quality — not an afterthought. Protection is matched to the part's finish, fragility, and shipping route.
Parts are wrapped individually so finished and cosmetic surfaces do not contact one another.
Cut foam and nesting cushion parts against shock and vibration during transit.
Soft interleaving and careful handling protect anodized and cosmetic aluminum faces.
Peel-off film shields A-surfaces and polished faces until the parts reach your line.
Dividers separate parts so edges and corners cannot rub or impact each other.
Sturdy, right-sized cartons with edge reinforcement resist crushing in the supply chain.
Palletized and reinforced packing for international freight and multi-handling routes.
Desiccant and sealed wrapping are added where humidity or long transit risk corrosion.
Quality workflow
From drawing to shipment, quality at every step
A single controlled flow carries your part from RFQ to dispatch, with a defined checkpoint at each stage.
- 01 Customer drawing
Drawings, 3D models, tolerances, alloy, and finish requirements received.
- 02 Engineering review
DFM and inspection planning — critical features and datums identified.
- 03 Material verification
Alloy and temper confirmed against certified stock.
- 04 Production
Controlled setups, tooling, and machining to the defined process.
- 05 In-process inspection
Critical features gauged during the run to hold consistency.
- 06 Final inspection
Dimensions, threads, finish, and cosmetics verified and recorded.
- 07 Packaging
Wrapping, foam, partitions, and protection matched to the part.
- 08 Shipment
Documented, protected, and dispatched to your receiving team.
Confidentiality & NDA
Your drawings stay yours
Confidentiality is standard, not a premium. Here is exactly how your files are handled.
CAD files and engineering drawings are handled confidentially.
- Your files are used only for engineering review, quotation, manufacturing, and quality inspection.
- We do not share customer drawings with third parties.
- A signed NDA is available on request before you send your files.
Related resources
Go deeper on how we machine and finish aluminum
The quality system sits on top of our machining, materials, and finishing work — explore the detail behind each.
Engineering capabilities
3, 4, and 5-axis milling, turning, tolerances, and the machining behind the inspection.
Open engineering capabilities Aluminum CNC machining servicesThe full range of aluminum parts we machine — housings, brackets, shafts, manifolds, and more.
Open aluminum cnc machining services Aluminum materials hub6061, 7075, 2024, 5052, and MIC-6 machining guides and material selection.
Open aluminum materials hub Aluminum surface finishes hubAnodizing, blasting, brushing, and laser marking, with quality trade-offs for each.
Open aluminum surface finishes hub Industries we serveHow our quality system supports robotics, medical, aerospace, electronics, and industrial work.
Open industries we serve Custom aluminum CNC partsDrawing-built aluminum components for prototypes, spares, and recurring production.
Open custom aluminum cnc partsJump to a product: aluminum housings & enclosures, brackets & mounts, shafts & bushings, manifold blocks, and fixtures & tooling. By industry, see robotics, medical devices, aerospace tooling, electronics housings, and industrial equipment.
Put our quality system to the test
Send your drawings and inspection requirements. We review manufacturability, define the inspection plan, and reply with next steps within one business day.
- ISO 9001 quality management
- Material certificates available
- FAI reports available
- Engineering review within one business day
- NDA available on request