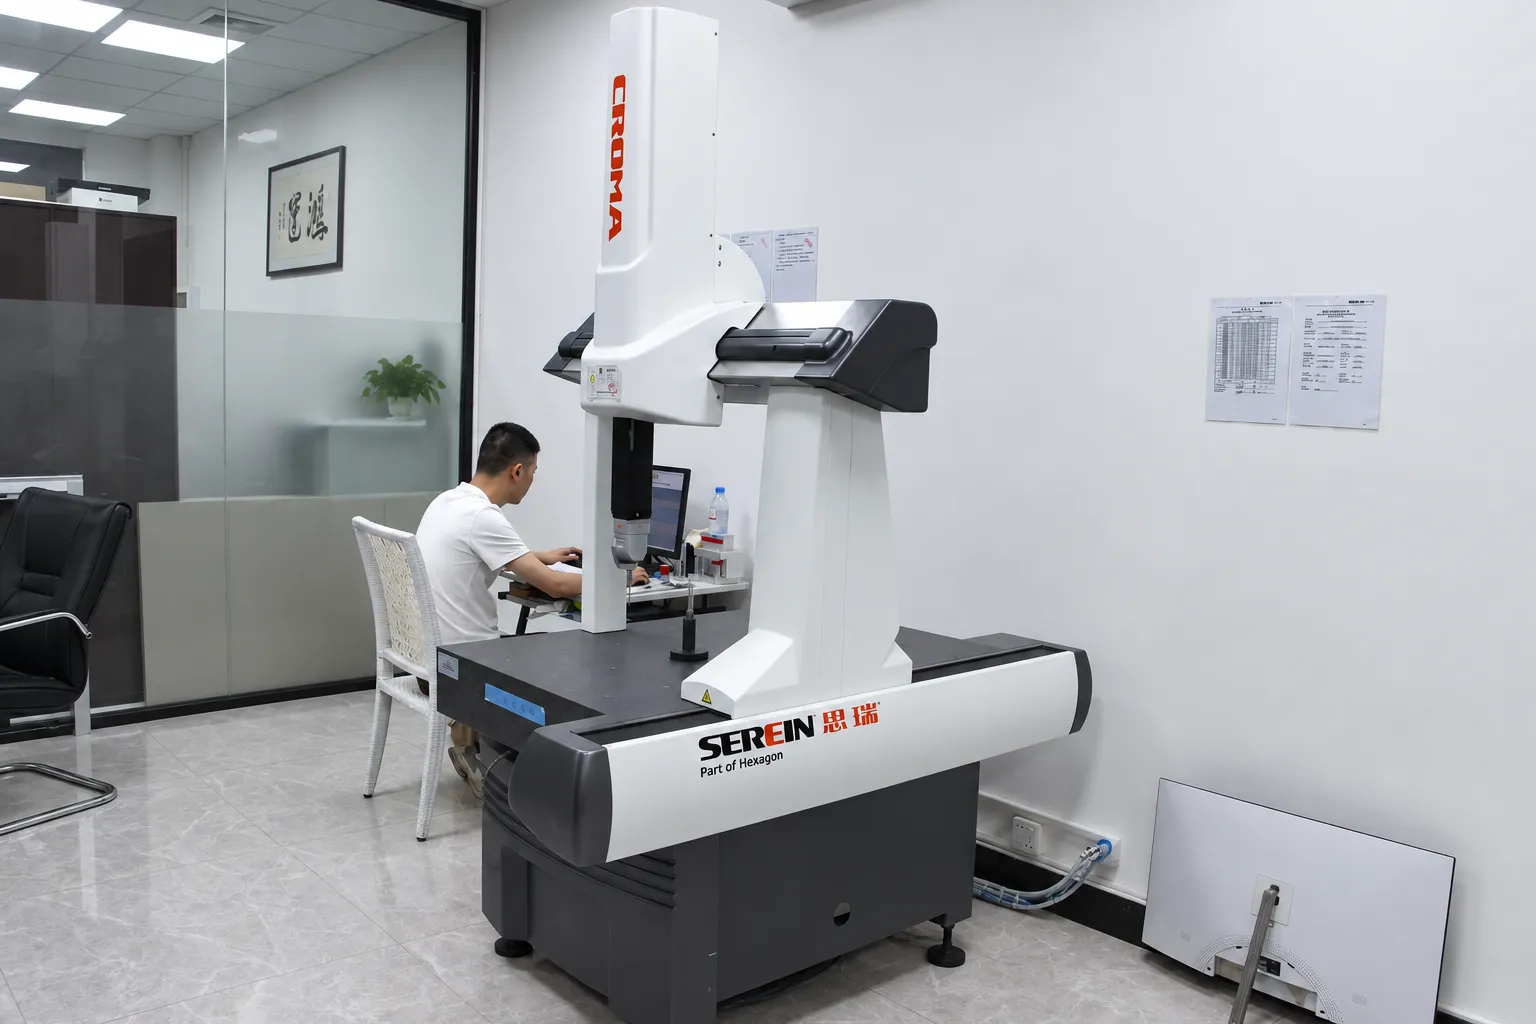
A measuring room separated from the machining floor, with instruments on a calibration schedule, is the difference between a dimension that is measured and one that is estimated.
Inside the factory
Inside Our Aluminum CNC Machining Facility
Sourcing aluminum parts from overseas means trusting a shop you have not walked through. This page is the walk-through: the machining floor, the measuring room, the tool room, the finishing bench, and the sample cabinet, photographed as they are.
Our works are in Qingxi, Dongguan, in Guangdong province. If you want to see something that is not on this page, ask and we will photograph it.
- ISO 9001:2015 certified
- Machining, inspection and finishing under one roof
- RFQ answered within one business day
Machining floor
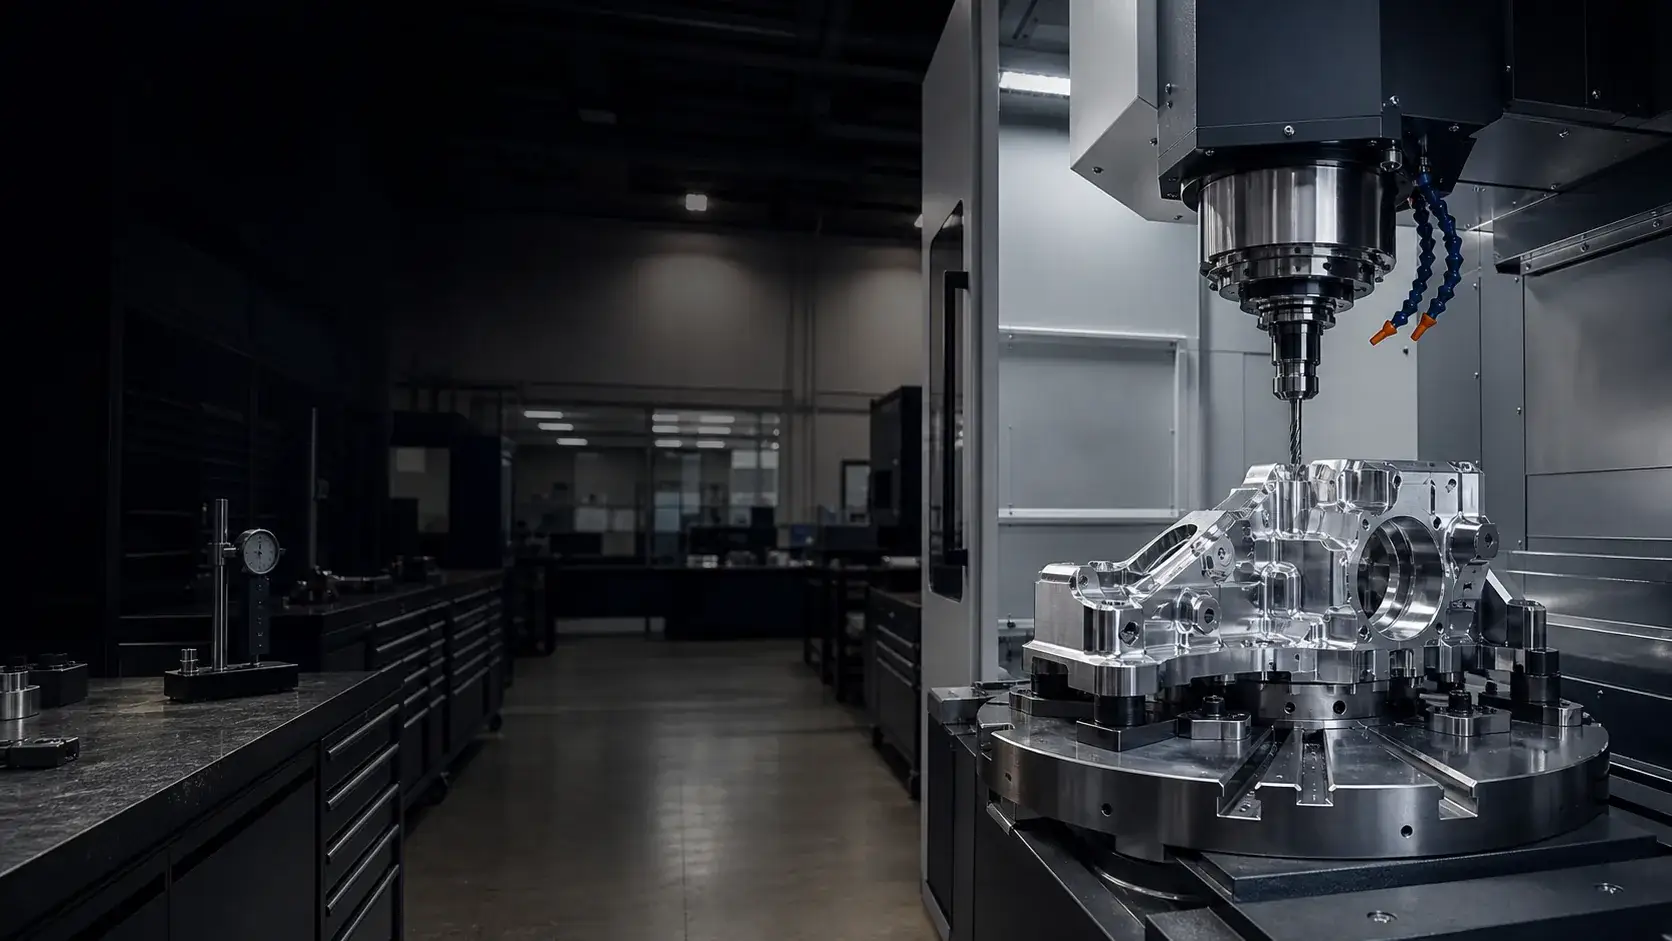
Vertical machining centers running aluminum
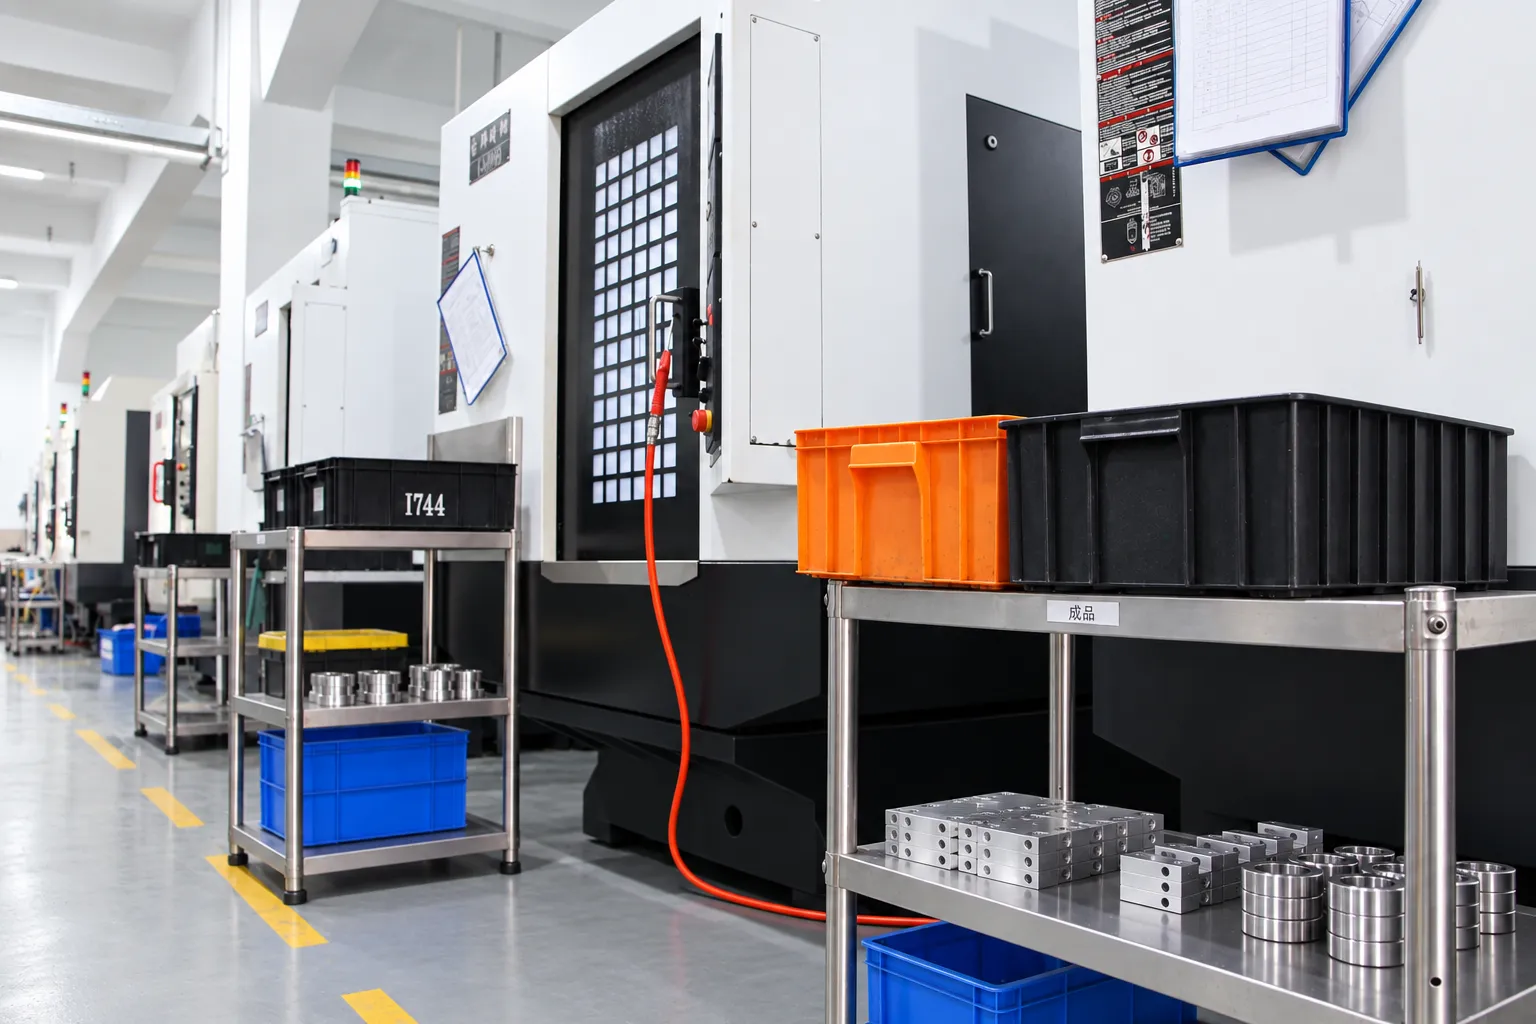
Aluminum milling is the core of the shop. Work moves between machines in bins rather than sitting in a queue, which is what keeps prototype batches and small production runs on the same floor without one starving the other.
Most jobs are proved out on the first part before the run is released. For the process detail behind that — the alloys, the tolerance bands, the secondary operations — see the capabilities page.
Inspection
A measuring room, not a bench in the corner
Dimensional inspection runs in its own room, away from the coolant and the vibration of the floor. A coordinate measuring machine handles true position, profile and flatness; an optical system covers small, thin and delicate features a contact probe would move.
What that produces for a buyer is a dimensional report tied to the drawing, and first article inspection on a first production lot.
Tooling
Cutter condition is managed, not assumed
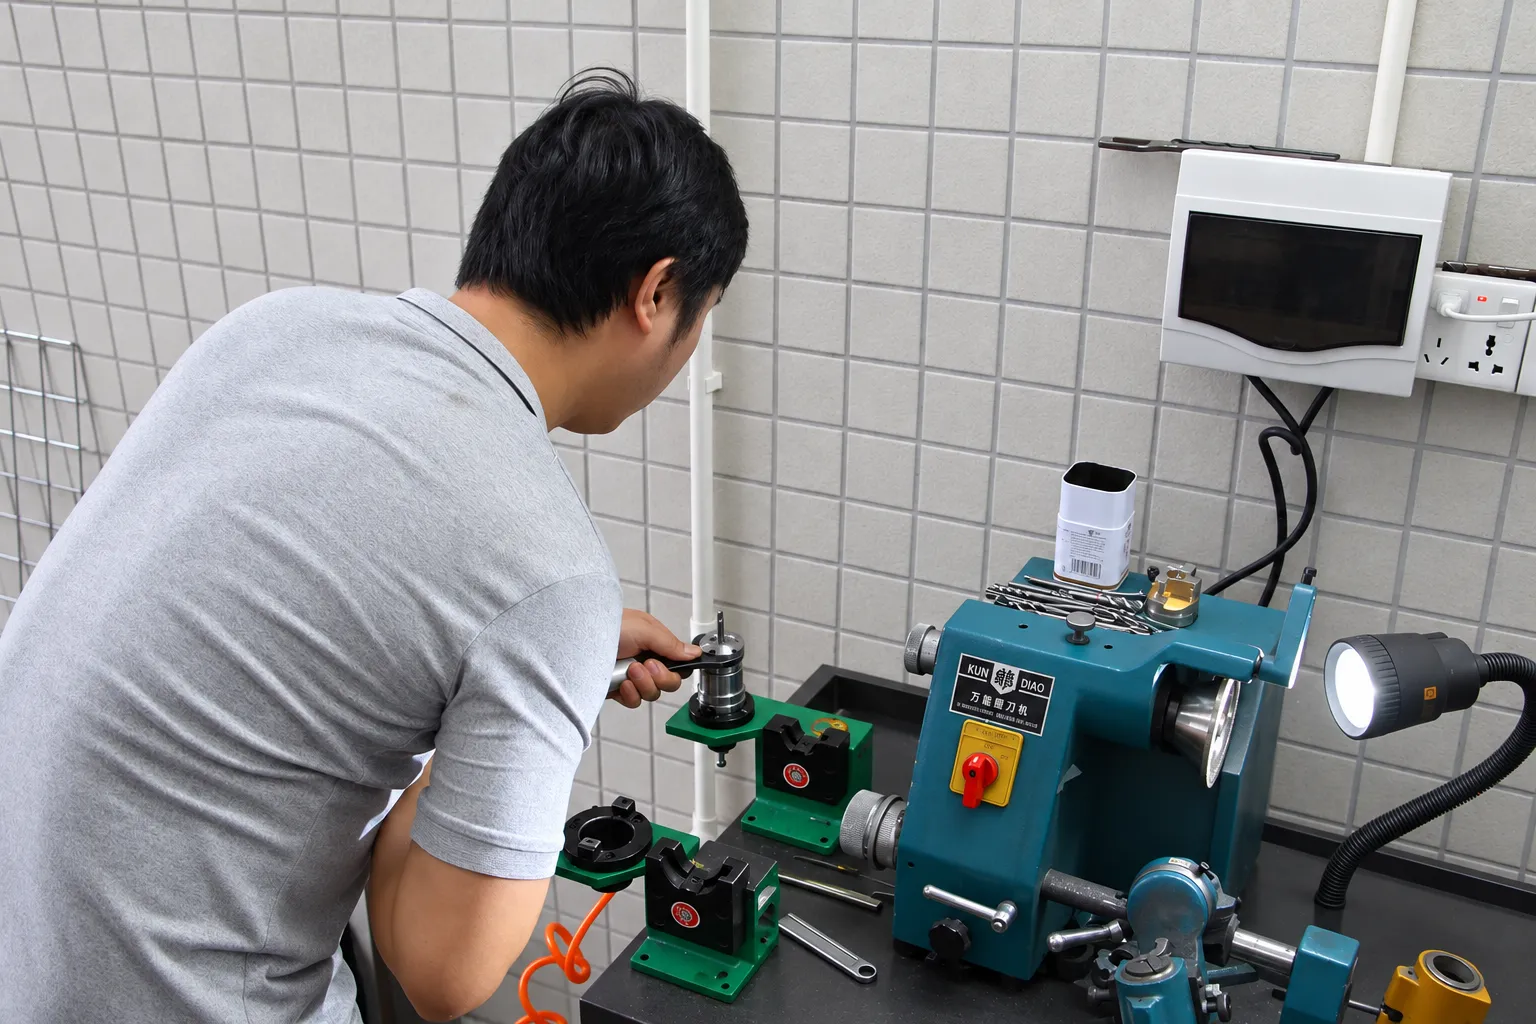
Tool regrinding is done in-house. That matters more on aluminum than people expect: a worn edge does not usually break the part, it quietly changes the surface finish and the size, and the first sign is a cosmetic rejection two weeks later.
Keeping regrinding on site means a tool comes out of service when it should, rather than when a replacement arrives.
Finishing
Deburring and blasting before the part leaves
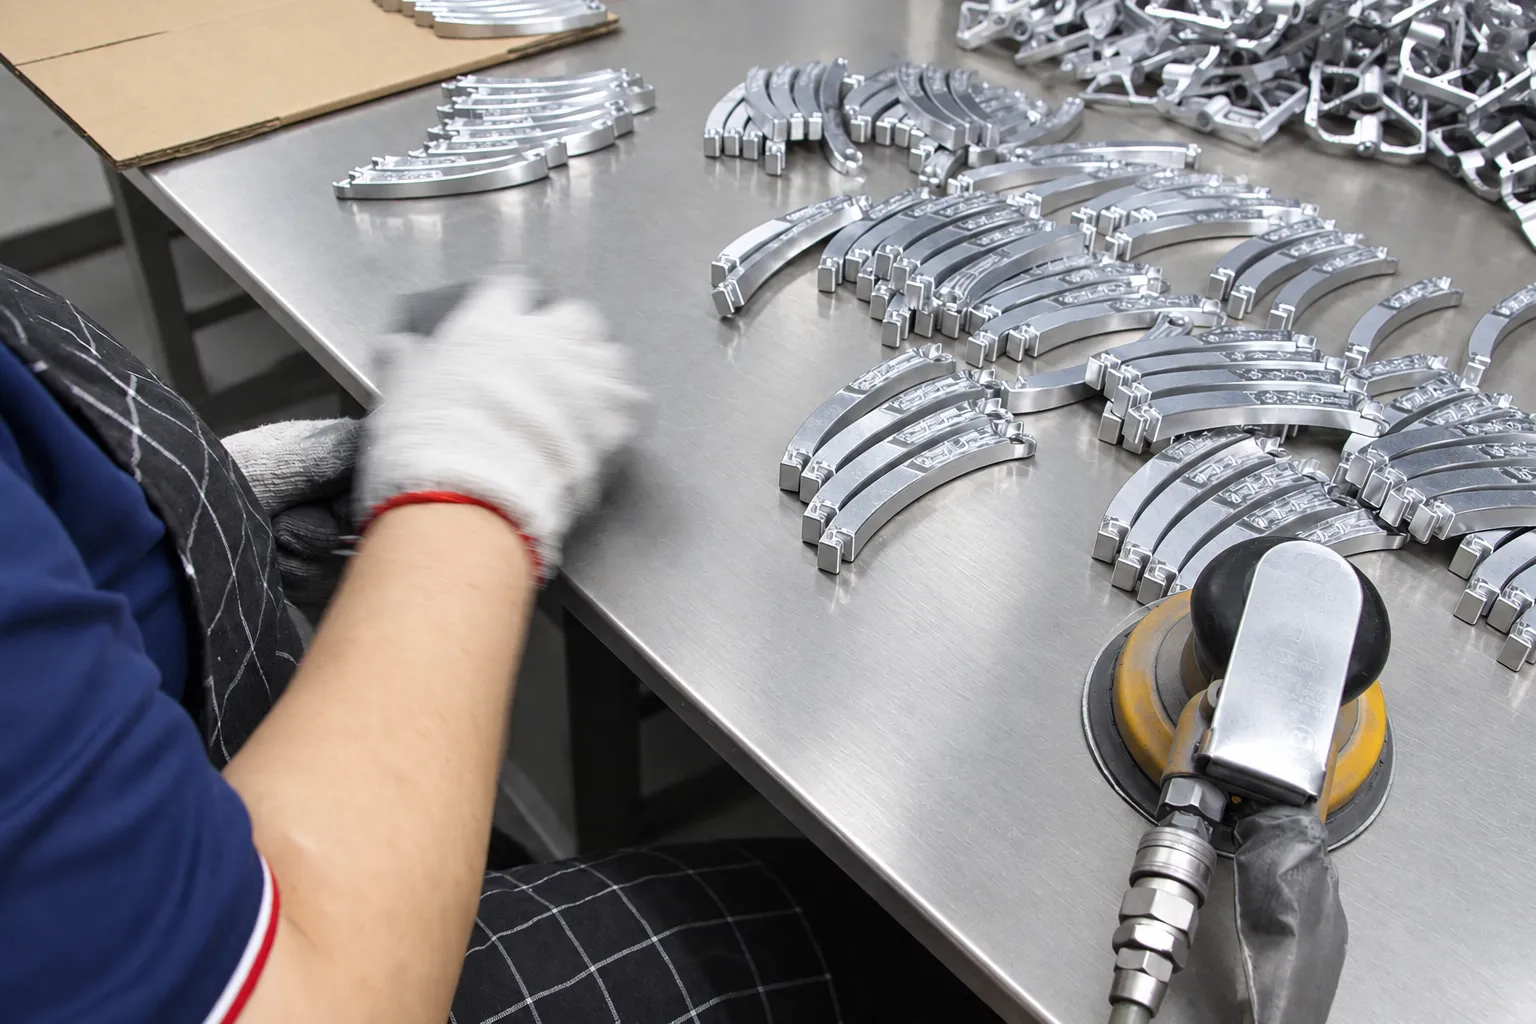
Deburring, polishing and bead blasting run on site. On an anodized part this is the half of the appearance that is decided before the tank — the blast grit sets how matte the finish reads, and the film only makes it permanent.
Anodizing and plating are done by our finishing partners to a named specification, with the surface preparation controlled here first.
Sample library
Parts we have already made
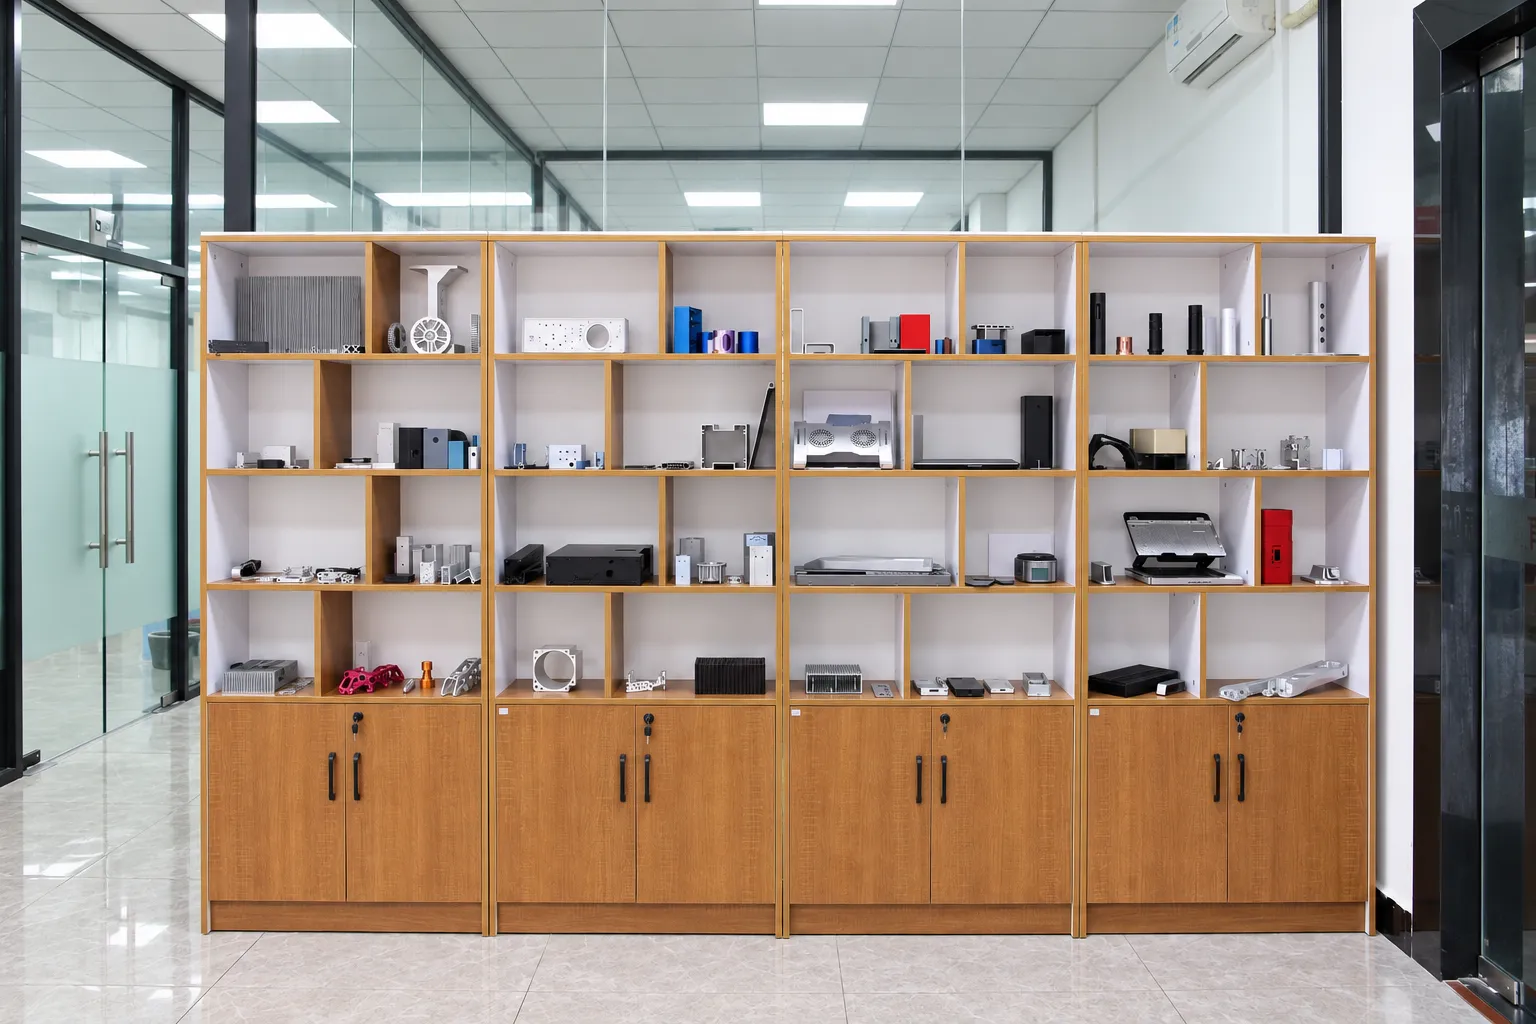
The sample library holds production parts from past programs — housings, heat sinks, brackets, plates and turned components across the alloys and finishes we run most often.
It is the quickest way to settle a finish or texture question: rather than describing a result, we send a photograph of a part that already has it.
Before you order
What to ask a shop you cannot visit
These are the questions worth asking any overseas supplier, including us. A shop that cannot answer them quickly is telling you something.
Anything sent out adds a handover. Ask which steps are on site and which go to a partner, and make sure the outside ones are named on the purchase order by specification.
A photograph of a part already made in the alloy and finish you need settles more than any capability list. That is what the sample library is for.
Next step
Send a drawing and see what comes back
Upload the CAD and the print. You will get an engineering review — alloy, tolerances, finish and the questions a quote depends on — within one business day.